Printing Interlocking Chainmail Armor That Flexes Without Cracking
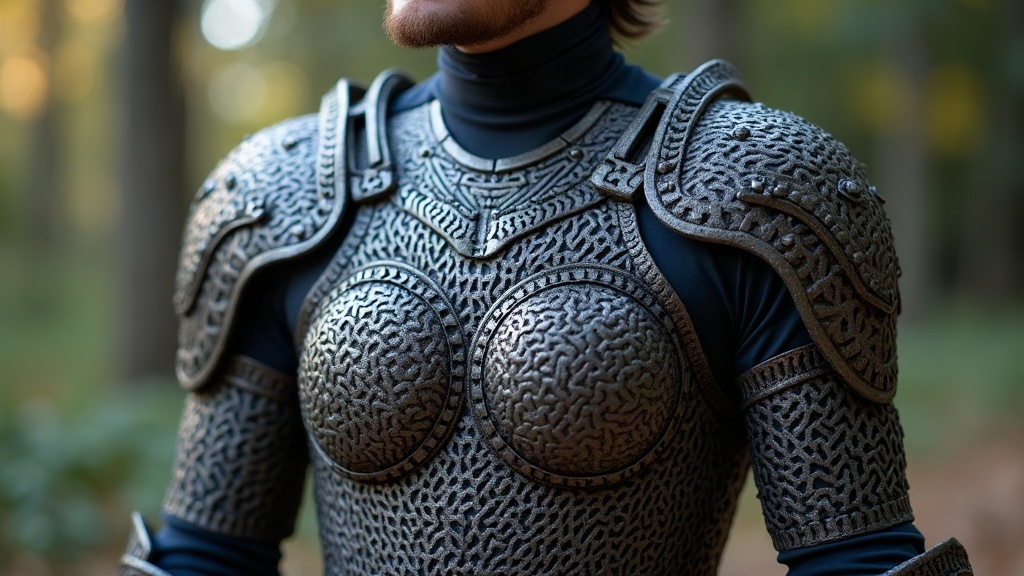
Why Most Printed Chainmail Fails
Chainmail is basically thousands of tiny hinges stacked together. Every ring has to twist a little against its neighbors every time the wearer moves, and that’s where most prints fall apart, literally.
- Rigid filament under repeated flexing. PLA, even PETG, will survive one bend just fine. But cyclic flexing (walking, raising an arm, just sitting down) fatigues the ring at its thinnest point, and eventually it snaps clean along a layer line. Not a slow tear. A crack.
- Zero clearance between links. Print-in-place chainmail only works if there’s an actual air gap between interlocking rings. Fuse adjacent rings even slightly during printing and the “joint” turns into a solid blob. No rotation, no flex. It cracks the first time someone forces it to move.
Fix both at once: pick a flexible material, and give every ring real, deliberate tolerance.
Choosing the Right Filament
Not every filament labeled “flexible” behaves the same when it’s locked into a ring.
- TPU (95A shore hardness) is the default for a reason. Elongation at break often runs 400-600%, and it shrugs off fatigue cracking in a way rigid plastics simply can’t. It’s the closest plastic analog to how real steel mail moves.
- TPU 85A is softer, drapes more like actual fabric. Great for mail meant to hang over shoulders naturally, but it can feel too floppy for anything load-bearing, like a gauntlet that needs to hold its shape.
- PETG should stay off the table for load-bearing mail. It’ll take a few flex cycles, sure, then fail with a sharp, brittle snap instead of tearing gracefully like TPU does.
- Nylon gives you rigidity with a bit of give, but it’s needy: careful drying beforehand (more on that below), higher nozzle temps, and a tendency to warp thin rings if you’re not watching it.
For most cosplay builds and functional armor, 95A TPU is the sweet spot between flex and structure.
Designing Rings for Flexibility
Material gets you halfway there. Geometry does the rest.
Clearance Tolerance
Build in 0.3-0.5 mm of clearance between one ring’s inner surface and the outer surface of the ring locked inside it. Go tighter and the printer fuses the joint shut. Go looser and the mail feels sloppy, rattles when you move. Print a 10-20 ring test strip first; clearance needs shift depending on your printer’s calibration and nozzle size, so don’t guess on a full panel.
Ring Cross-Section
- Round or D-shaped profiles flex more evenly than square ones. Square edges concentrate stress right at the corners, which is exactly where you don’t want it.
- Keep wall thickness in the 1.2-1.8 mm range. Go thinner and rings flex easily but wear out fast at contact points. Go thicker and you gain strength but stiffen the whole sheet, defeating the point.
- Round off internal corners wherever you can. Even a 0.5 mm fillet cuts stress concentration by a noticeable margin.
Weave Pattern
European 4-in-1 is the easiest pattern to print in place. It lays flat on the bed and barely needs support. Japanese and King’s weaves look sharper and more intricate, but more rings overlap at each junction, so bridging settings need extra attention or you’ll get sag and fused joints.
Print Settings That Prevent Cracking
- Layer height: 0.16-0.2 mm. Finer layers mean fewer weak points along the ring’s flex axis.
- Print orientation: Lay rings flat on the bed, loop horizontal, so layer lines run perpendicular to the main flex direction instead of parallel to it. This alone prevents a lot of snapping.
- Wall count: 3-4 perimeters minimum, skip sparse infill entirely. Rings need to be solid or close to it. Thin single-wall rings crack almost on contact.
- Cooling: Run the fan at full on TPU. It keeps rings from drooping or fusing to their neighbors mid-print, which matters a lot for keeping that clearance intact.
- Print speed: Drop to 20-30 mm/s for TPU. Push it faster and you get under-extrusion gaps, and those gaps become exactly where cracks start.
- Temperature: Stick to the lower end of your TPU’s range, usually around 220-230°C. Cooler prints give crisper joints with less stringing, and less stringing means rings don’t accidentally glue themselves together.
Testing and Post-Processing
Before you commit to a full panel, flex a test strip by hand, back and forth, 50 to 100 times. Watch for whitening (stress blanching) or any hint of a crack starting. See either one? Bump up wall thickness a bit, or try a softer shore hardness before scaling up to the full piece.
Some makers also lightly bead-blast or tumble the finished sheet. It knocks loose any micro-fused joints the slicer missed, freeing up rings that printed a touch tighter than planned.
Conclusion
Crack-resistant, genuinely flexible 3D printed chainmail is absolutely doable. It just comes down to matching the material’s elongation to real flex cycles, and building actual clearance into every single joint, not just hoping it works out. Start with 95A TPU. Design rings with 0.3-0.5 mm clearance and rounded cross-sections. Print slow, cool it fully, and always test a small strip before scaling to a full armor panel. Skip any one of these and you’ll get mail that looks flawless fresh off the bed, then falls apart within a day of actual wear.