Designing Snap-Fit Enclosures for Raspberry Pi Zero 2 W Boards
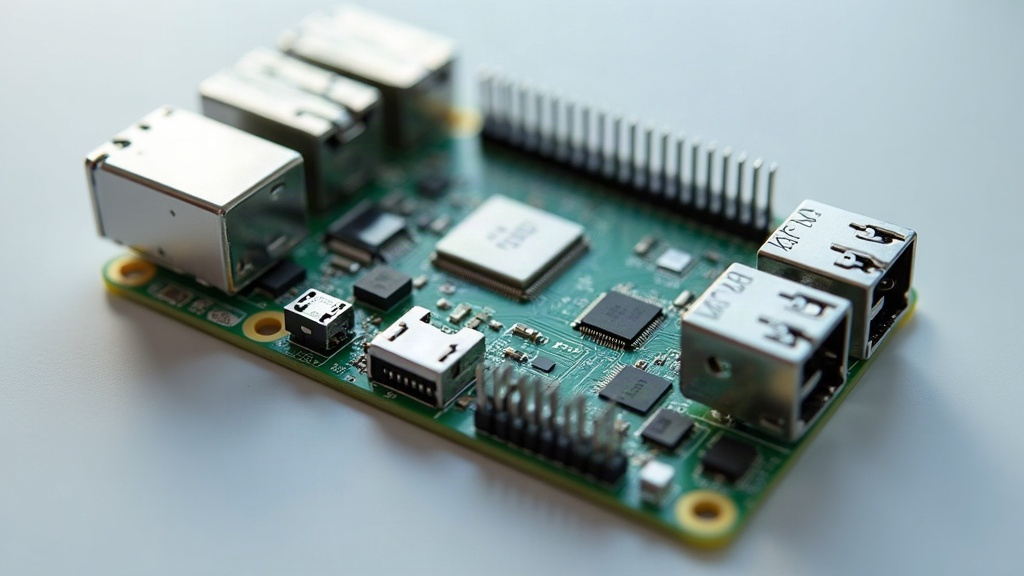
Know Your Board Before You Draw
Every measurement here matters. Get it wrong and your snap-fit case will either crush the board or rattle around it like a loose tooth.
- Bare board footprint: 65 mm × 30 mm, about 5 mm thick.
- Mounting holes: four M2.5 holes on a 58 mm × 23 mm rectangular pattern.
- Tallest components: the micro-USB ports and micro-HDMI connector, sitting roughly 5 to 6 mm above the PCB surface.
- GPIO header: solder on a 2×20 pin header and you’ve just added about 8.5 mm of extra height. Plan a cutout or a raised lid section for it now, not after your first print fails to close.
Don’t trust the spec sheet blindly. Pull out a set of calipers and measure your actual board. A few tenths of a millimeter of extra overhang on a USB port, or a slightly taller header than expected, and your snap hooks end up landing in the wrong spot.
Choose the Right Snap-Fit Geometry
For a small, thin-walled enclosure like this one, the cantilever snap does most of the work. Picture a thin beam with a hook on the tip: it bends out of the way as the two halves come together, then springs back once the hook clears the ledge.
- Beam length-to-thickness ratio: aim for roughly 5:1 to 10:1. So a 1 mm thick beam should run somewhere between 5 and 10 mm long.
- Undercut (hook depth): 0.4 to 0.6 mm is plenty for PLA and PETG. It’s tempting to go deeper for a “more secure” look, but that just piles stress at the base of the beam, and that’s exactly where it snaps off.
- Deflection: the required deflection roughly equals your undercut depth. Keep it under about 1.5% of the beam’s length if you’re using a stiffer plastic.
- Draft angle: add a 30 to 45 degree lead-in chamfer on the hook so the halves glide together instead of jamming.
- Root fillet: a small radius at the base of each cantilever goes a long way. Sharp inside corners are basically where every broken snap beam starts.
A layout that works well for beginners: two cantilever snaps on each short edge, plus two simple locating tabs on the opposite side. Four flexing points, firm closure, nothing overengineered.
Design the Case Around the Board, Not the Other Way
Start with the board itself and build the enclosure outward from there, not the reverse.
- Wall thickness: 1.2 to 2.0 mm strikes a decent balance between rigidity and printability at this scale.
- Internal clearance: leave 0.2 to 0.3 mm of space around the board so it drops in without you having to force it.
- Snap engagement: give the mating surfaces of the two halves about 0.2 mm of clearance, but keep the hook and its ledge sharp and well-defined.
- Port openings: cut rectangular openings for USB and HDMI with roughly 0.3 mm of extra room so cables plug in cleanly instead of scraping plastic every time.
- Ventilation: if your Pi runs hot under load, add a few slots or small holes. A fully sealed shell traps heat, and nobody wants their board throttling inside a plastic box.
Material Choice Decides Whether the Clips Survive
- PETG: the all-around winner here. It flexes without cracking and shrugs off dozens (even hundreds) of open/close cycles far better than PLA. If this is a case you’ll actually open regularly, use PETG.
- PLA: okay for a prototype or a case that just sits on a shelf, but the snap beams tend to snap (fittingly) after a handful of aggressive cycles, especially in a cold room.
- ABS/ASA: tough and springy in theory, but they warp easily mid-print, and warping throws off your snap alignment fast. Only worth it if you have an enclosed printer and solid bed adhesion dialed in.
For your first working case, print in PETG with 3 to 4 perimeters and 20 to 25% infill. And make the snap beams solid, no infill pattern inside them. That one detail probably matters more than anything else on this list for how long your clips last.
Print Orientation Makes or Breaks Snaps
Layer lines are the weak link in any FDM print, and a snap beam that flexes across those lines is asking for trouble.
- Print cantilevers lying flat on the build plate, not standing up. A vertically printed beam will delaminate along its layer lines the very first time you flex it.
- 0.2 mm layer height gives a solid balance of speed and strength. Drop to 0.12 mm if you want crisper snap ledges, but expect a longer print time.
- Print the case halves face-down. You get the cleanest exterior finish, and the snap geometry needs the least support material.
- Turn off supports anywhere near the snap features. Support scars on a beam that’s meant to flex are basically pre-cracked stress points.
Test prints cost almost nothing. Print just the snap tab as a small standalone coupon, flex it ten times by hand, and tweak the undercut or beam length before committing to a full print run.
Conclusion
Boil it all down and a reliable snap-fit enclosure for the Pi Zero 2 W comes from three things: accurate board measurements, conservative cantilever geometry, and PETG printed with the flex direction parallel to the bed. Keep your undercuts at 0.4 to 0.6 mm, throw in lead-in chamfers and root fillets, and give the ports a little breathing room. Get those basics right and you end up with a case that snaps shut with a satisfying click, pops open whenever you need it to, and holds up over hundreds of cycles. No screws, no glue, no drama.